Table of Contents
- Introduction
Key Takeaways
- Industrial conveyor rollers minimize resistance, enabling smoother product transfer and faster cycle times in manufacturing.
- Choosing the right industrial conveyor roller can reduce downtime and improve overall equipment effectiveness (OEE).
- Quality rollers from a reliable industrial conveyor roller manufacturer ensure precision and longevity, leading to reduced maintenance costs.
- Roller applications range from assembly to packaging, enhancing efficiency in various sectors including automotive and e-commerce.
- Collaboration with an experienced industrial conveyor roller manufacturer helps optimize roller selection based on specific operational needs.
Conveline Systems Pvt. Ltd. is a Leading Manufacturer of Industrial Conveyor Rollers.
In high-speed manufacturing, every second of idle time costs money. Industrial conveyor rollers are the quiet workhorses that keep products moving, lines balanced, and throughput predictable. When chosen and applied correctly, they reduce manual handling, lower wear on belts and drives, and help plants meet tight delivery windows without compromising safety. This guide explains why rollers matter, where they fit in modern plants, and how to select the right set-up for your line.
Why rollers matter in modern manufacturing
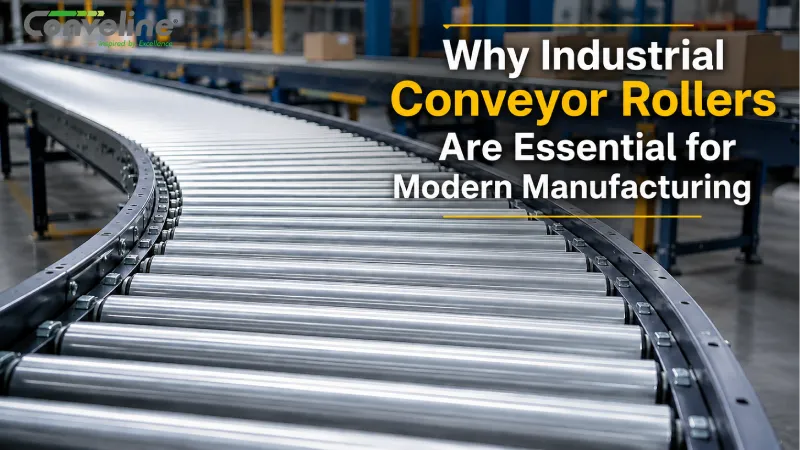
Rollers turn friction into controlled motion. By supporting loads on rotating cylinders, they minimize resistance and allow smooth transfer between stations. The result is faster cycle times, fewer jams, and more consistent product orientation. In automated and semi-automated lines, rollers also enable accumulation, merging, and gentle product handling—critical for fragile packs, irregular shapes, and high-mix production.
Plants that standardize on quality rollers see tangible gains: reduced downtime from roller failures, lower maintenance frequency, and better energy efficiency on powered sections. For an Industrial Conveyor Roller Manufacturer, the focus is on precision tolerances, robust sealing, and materials that match the environment—whether that is food-grade stainless, corrosion-resistant plating, or chemical-resistant polymers.
Where conveyor rollers are used in manufacturing plants
Roller-based conveyors appear across the value chain. Common use cases include:
- Raw material intake and staging – Gravity rollers move pallets, totes, and drums from receiving to staging areas with minimal effort.
- Assembly and sub-assembly lines – Powered rollers drive cartons and kits between workstations while allowing operators to accumulate items without back-pressure.
- Packaging and Labeling – Rollers maintain consistent spacing for labellers, coders, and shrink wrappers, improving scan rates and reducing rework.
- Quality inspection and sorting – Low-friction rollers enable smooth rotation and indexing for cameras, checkweighers, and sortation gates.
- Warehousing and dispatch – Tapered and curved rollers guide products around bends and merges, supporting high-throughput order fulfilment.
These applications range from automotive to fast moving consumer goods, pharma, e-commerce logistics, packaging, and manufacturing in general. The appropriate choice of roller in terms of tube material, diameter, bearing type, and finish will impact reliability in each situation.
How rollers improve efficiency and reduce downtime
Efficiency gains come from three areas:
- Lower friction and smoother flow – Precision bearings and balanced tubes reduce resistance, allowing lighter drives and smoother transfers.
- Modular maintenance – Individual rollers can be swapped quickly without stopping the entire line, cutting mean-time-to-repair.
- Scalability – Roller sections can be added or reconfigured as product mixes change, supporting flexible manufacturing without major re-engineering.
For plants running multiple shifts, these advantages compound. Fewer stoppages mean higher overall equipment effectiveness (OEE), and standardized roller dimensions simplify spares management.
Selecting the right rollers for your line
Selection starts with the application. Ask:
- What is the maximum load per roller and the total conveyor load?
- What product dimensions and bottom surfaces will contact the rollers?
- Is the environment dry, washdown, cold storage, or dusty?
- Do you need accumulation, merging, or precise spacing for automation?
A seasoned Industrial Conveyor Roller Manufacturer will suggest tubes made up of appropriate material, suitable bearing seals, shaft sizes, and mounting types in accordance with the above-mentioned parameters. For instance, in case of food and pharmaceutical applications, the use of stainless-steel rollers with improved seals is preferred.
Why quality and local manufacturing count
Rollers that are out of round, inadequately sealed, and not correctly sized to carry the load will give rise to problems related to tracking, noise generation, and early bearing wear. Custom made rollers reduce delivery time and are easier to customize and service. Conveline Systems Pvt.Ltd. is a large manufacturing company based in Ahmedabad, Gujarat, with substantial annual output capability, all manufactured in India.
Collaboration with a well-known Industrial Conveyor Roller Manufacturer is an excellent way to benefit from application experience. This includes everything from design reviews to spacing calculations to ensure that you don’t incur needless costs in the form of trials and errors.
Why Choose Conveline Systems Pvt. Ltd.?
Conveline Systems Pvt. Ltd, merges application engineering, in-house production, and on-field support services to offer rollers that work seamlessly every day. Our rollers are designed in such a way that they suit any practical situation, whether under changing loads, start-stop cycle, tough environment or not. We work hand-in-hand with our clients in the specification, layout verification, and supply of spares.
Conclusion
Rollers used in industrial conveyors are indispensable in current manufacturing operations since they make intricate material movement effortless. Choosing the appropriate rollers optimizes the flow process by minimizing manual labor and maintenance expenses in assembly, packaging, testing, and storage processes. There is a broad choice of rollers from basic to advanced designs that enable manufacturers to choose specific rollers based on their exact requirements. Cooperation with a reputable Industrial Conveyor Roller Manufacturer guarantees accuracy, quality material, and assistance that is important for continuous operation of the assembly line. At Conveline Systems Pvt.Ltd., our main priority is to use an engineering approach that will move your products smoothly and in time.
Need help selecting rollers or upgrading your line? Speak with our team for application advice, drawings, and roller specifications. Call us: +91 7486023925 or email info@conveline.com — and let Conveline Systems Pvt. Ltd. put your stock within reach.
FAQS

industrial conveyor rollers conveyor roller manufacturer manufacturing automation material handling gravity roller conveyor powered roller conveyor intralogistics warehouse automation production line efficiency Industrial Conveyor Roller Manufacturer

